10 Manufacturing ERP Capabilities to Test in One Order
10 Manufacturing ERP Capabilities to Test in One Order. Use a worked factory scenario, explicit inputs and exception checks before rollout.
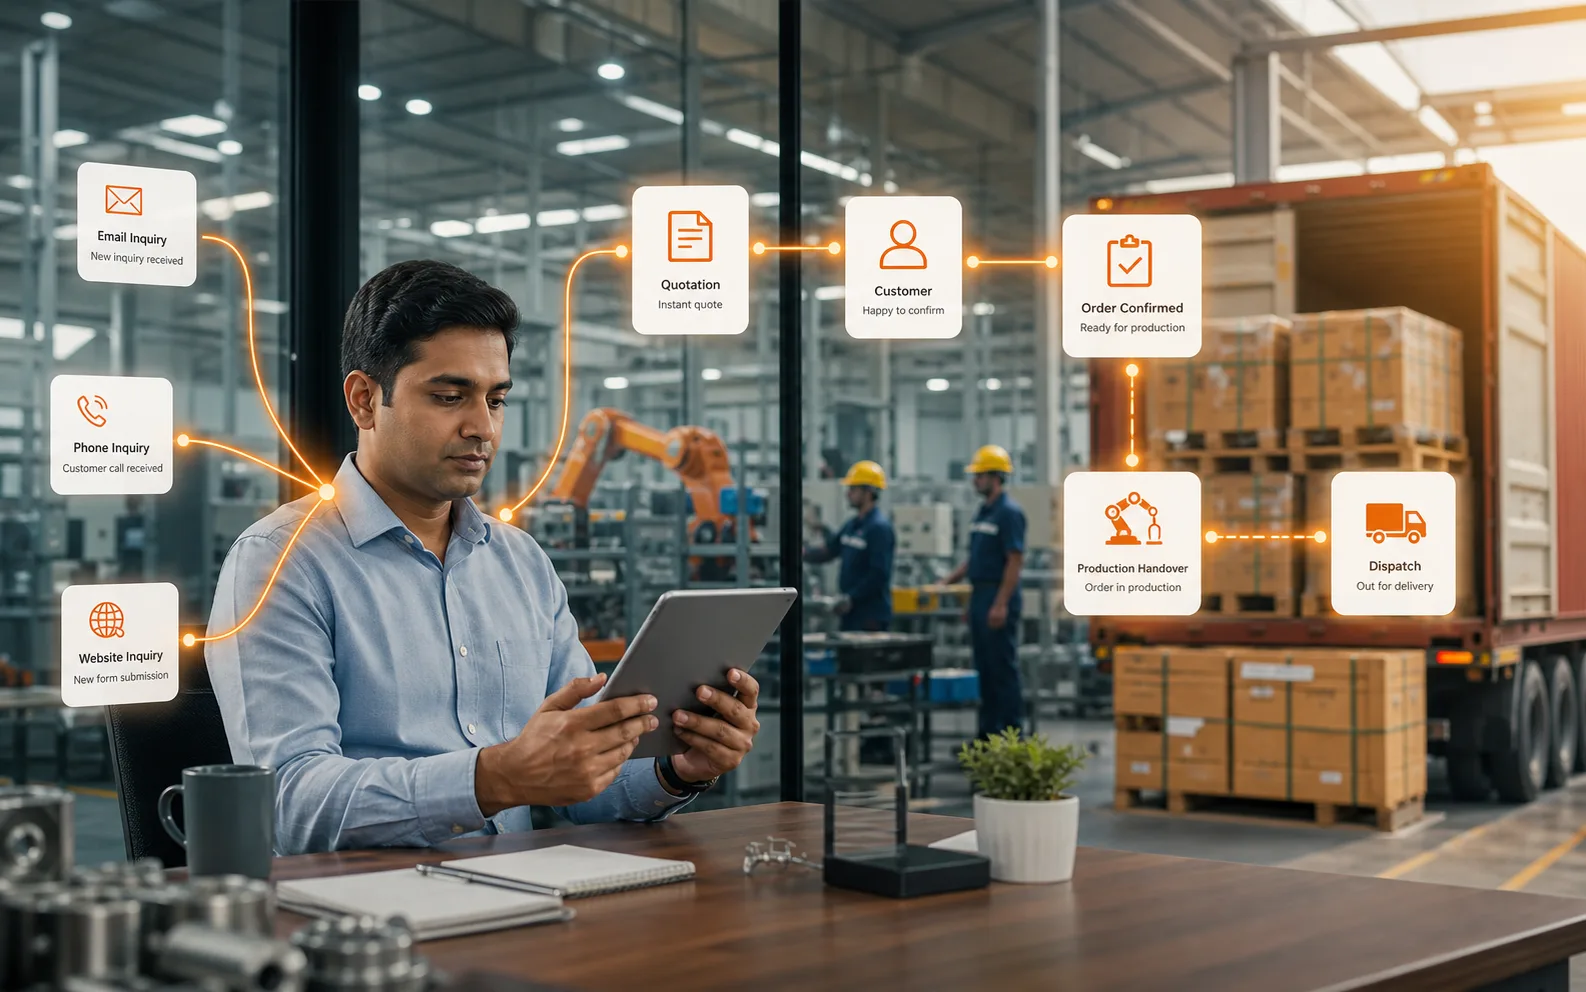
10 Manufacturing ERP Capabilities to Test in One Order helps you verify ten connected capabilities without relying on a checklist alone. Use a representative order, the people who perform the work and at least one difficult exception.
Run one order through quotation, BOM, material planning, purchase, receipt, production, inspection, finished stock, dispatch and management review.
Define the decision and its evidence
A connected test exposes handoff gaps that separate feature names cannot show.
We connect nested BOMs, routing, machine and worker entries, material consumption, rework, inspection and finished-goods receipt to the manufacturing order.
ISA-95 is the external process or vendor reference used for this guide. Vendor documentation records the vendor's stated workflow; our product statements come from our current product record.
| Step | Required input | Evidence to capture |
|---|---|---|
| 1 | Order, product and revision | Named owner and definition |
| 2 | Stock, suppliers and capacity | Current source record |
| 3 | Roles, permissions and approvals | Acceptance rule |
| 4 | Expected records at ten handoffs | Correction and escalation |
Run the workflow with accountable roles
- 1. Order, product and revision. Name the role that owns this record and decision.
- 2. Stock, suppliers and capacity. Use a current value from the representative order.
- 3. Roles, permissions and approvals. Write the passing condition before the test.
- 4. Expected records at ten handoffs. Assign correction and escalation responsibility.
Reconcile the result by hand. When the system differs from the source record, classify the gap as master data, timing, transaction ownership, permissions or configuration before changing the process.
Test the exceptions that disrupt a normal day
- Receipt is partial: record the expected status, permitted action, approver, correction path and audit evidence.
- Material needs substitution: record the expected status, permitted action, approver, correction path and audit evidence.
- Output enters rework: record the expected status, permitted action, approver, correction path and audit evidence.
A quick normal transaction shows the main path. A controlled exception shows whether the configured workflow can survive real factory conditions.
Connect this task to the operating workflow
review the product workflow, check the connected module, prepare the supporting records, see the control step, read the related guide. Book a connected Optiwise demo and ask us to run your scenario with the normal path, exception and correction.
Questions to settle during the demo
What should we prepare?
Prepare one representative order, the four inputs above and one complication your team encounters today. Remove confidential values while keeping the record relationships intact.
What is a passing result?
Accept the workflow when the normal path and exceptions leave a complete, role-appropriate record another person can reconcile. Validate the configured capability separately from any proposed commercial or operational outcome.
Choosing a manufacturing ERP is not the same as choosing ordinary business software. A factory has moving parts that generic tools often miss: BOMs, production stages, material shortages, QC hold stock, subcontracting, routing, batch movement, purchase planning, and dispatch commitments.
The right ERP should help the business run with fewer blind spots. The wrong ERP becomes an expensive data-entry layer that teams avoid.
Here are ten features manufacturers should check before selecting a system.
1. Manufacturing-Specific BOM Management
The ERP should support bills of material that match the way products are actually made. For complex products, multilevel BOM is essential. The system should handle components, subassemblies, scrap, alternatives, and revisions.
Without strong BOM control, MRP, costing, and production planning will all suffer.
2. Material Requirements Planning
MRP helps calculate what material is needed based on demand, BOM, stock, open purchase orders, and lead times. This feature is critical for reducing shortages and avoiding overbuying.
Look for shortage reports, purchase suggestions, planned requirements, and visibility into open orders.
3. Inventory and Warehouse Control
Manufacturers need inventory visibility by item, warehouse, status, batch, and sometimes serial number. The ERP should support GRN, stock transfer, issue to production, physical reconciliation, minimum and maximum stock levels, and rejected or hold stock.
Stock accuracy is the foundation of planning.
4. Production Planning and Work Orders
The ERP should help convert demand into work orders, check material availability, schedule production, and track status. It should make the plan visible to production, stores, purchase, and management.
A good system should show what is planned, what is running, what is delayed, and what is blocked.
5. Routing and Process Tracking
Routing defines operations, sequence, work centres, and time. This helps with capacity planning, costing, and shop floor tracking.
If the ERP cannot represent the production process, it will struggle to support real factory execution.
6. Quality Control Workflows
QC should cover inward inspection, in-process checks, final inspection, rejection reasons, and corrective actions. QC status should affect stock availability so rejected material is not used accidentally.
Quality data should also support supplier rating and customer complaint analysis.
7. Purchase and Supplier Management
Purchase features should include RFQ, quote comparison, purchase orders, approvals, supplier ratings, GRN linkage, purchase returns, and invoice validation.
This helps control procurement cost and vendor reliability.
8. Sales, Dispatch, and Customer Commitments
ERP should connect sales orders with production and dispatch. Sales teams need visibility into stock, production status, delivery dates, and pending dispatches.
This improves customer communication and reduces unrealistic promises.
9. Finance and Accounting Integration
Manufacturers often use accounting systems such as Tally. ERP should support clean integration so invoices, payments, credit notes, debit notes, and accounting data flow properly.
This reduces duplicate entry and improves reconciliation.
10. Dashboards and Role-Based Visibility
Management needs dashboards for production, inventory, purchase, quality, receivables, payables, and dispatch. Users need role-based access so each team sees what matters without exposing everything unnecessarily.
Dashboards should come from live workflows, not manually prepared reports.
What Makes Optiwise Relevant
AICAN Optiwise is designed for manufacturing businesses that need connected workflows without unnecessary complexity. It brings purchase, inventory, production, QC, sales, and finance-related visibility into one operating system.
The goal is practical control: fewer missed updates, better planning, and clearer decisions.
How to Evaluate ERP Features
Do not evaluate features only from a sales demo. Ask how the system handles your real cases: partial GRN, QC rejection, subcontracting, multi-level BOM, urgent production, purchase return, credit note, stock transfer, and Tally integration.
A manufacturing ERP should survive real workflows, not just clean demo data.
Founder’s Note
At AICAN, we believe ERP selection should start with factory reality. If the system cannot handle how your material moves, how your products are built, and how your teams make decisions, it will not create control. Optiwise is built from that manufacturing-first view.
FAQs
What is the most important feature in manufacturing ERP?
There is no single feature for every business, but BOM, inventory, production planning, MRP, and QC are usually foundational.
Should ERP integrate with accounting software?
Yes. Integration reduces duplicate entry and keeps finance aligned with operations.
Why is BOM important in ERP?
BOM defines material requirements, supports costing, and drives production planning.
How should manufacturers evaluate ERP demos?
Use real scenarios from your factory instead of only watching standard demo flows.
Where can I learn more about AICAN?
Visit AICAN and About AICAN.
Related Posts
A Manufacturing Alternative to SAP: Optiwise
Run your factory in Optiwise, a manufacturing alternative to SAP Business One with connected operations, AI agents and no-code workflows.
14 Jun 2026Read more →How Do I Know If My Manufacturing Business Really Needs an ERP?
A practical guide for manufacturers to identify when spreadsheets, manual follow-ups, and disconnected systems are no longer enough — and when ERP becomes an operational necessity.
14 Jun 2026Read more →Production Management System Optimized | Optiwise
Learn best practices for optimizing a production management system across planning, scheduling, material readiness, quality, and reporting.
12 Jun 2026Read more →
What Is the Best ERP for Pharmaceutical Manufacturing?
Learn how to choose the best ERP for pharmaceutical manufacturing, with guidance on batch control, quality workflows, traceability, inventory, documentation, and GMP discipline.
10 Jun 2026Read more →