Improve OEE: Find the Loss Before Choosing the Action
Improve OEE. Use a worked manufacturing test, explicit inputs and exception checks before rollout.
Improve OEE: Find the Loss Before Choosing the Action helps you use availability, performance and quality losses without hiding the denominator. Test one real order and one exception before expanding scope.
For a 480-minute shift with 60 minutes planned stop and 45 minutes unplanned stop, use the agreed planned production time, actual run time, ideal cycle and good count. Keep setup, microstop, slow-cycle and rejection reasons separate.
Start with the decision the system must support
Calculate each component for one machine and shift, then investigate the largest named loss.
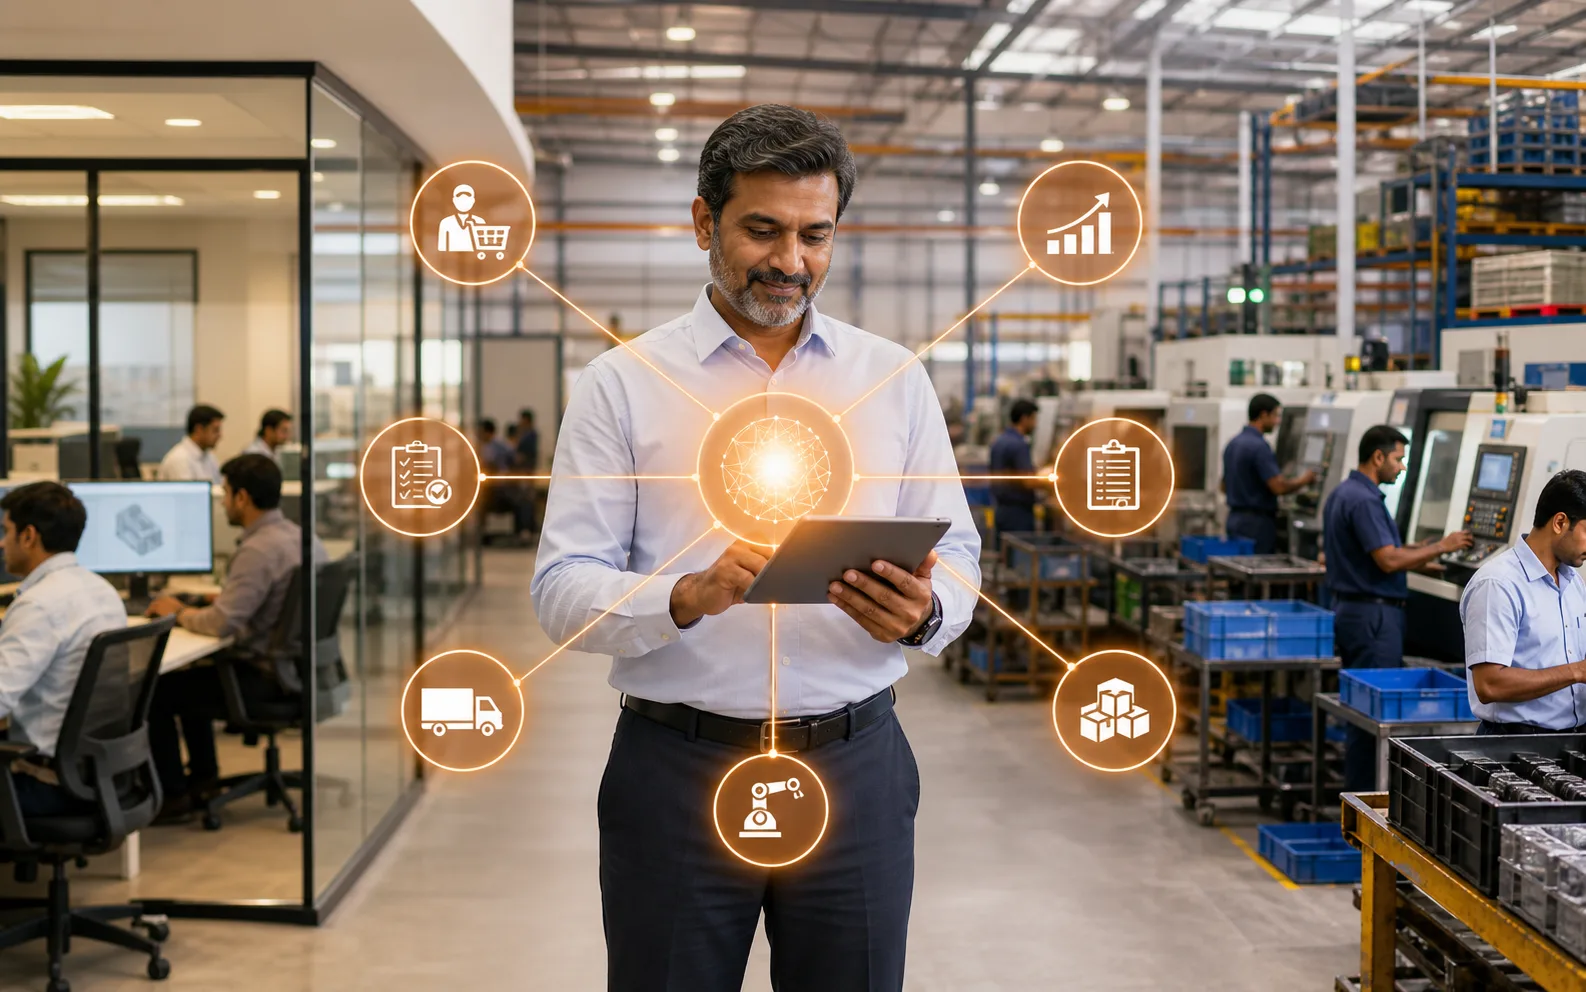
Optiwise IoT views include runtime, downtime, cycles, load, energy, OEE and multi-plant dashboards; production and quality records add the order and rejection context.
Use NIST Manufacturing Cost Guide as an external reference for the relevant process or control model. It does not prove an Optiwise feature or business result; our product statements come from the current feature record.
| # | Input to prepare | Evidence to retain |
|---|---|---|
| 1 | Planned production time | Owner and last update |
| 2 | Runtime and downtime reasons | Definition and source |
| 3 | Ideal cycle and total count | Acceptance rule |
| 4 | Good, reject and rework count | Exception owner |
Run one controlled workflow
- 1. Planned production time. Name the owner and authoritative record.
- 2. Runtime and downtime reasons. Use the current value from the test order.
- 3. Ideal cycle and total count. Write the pass condition before the demo.
- 4. Good, reject and rework count. Assign the person who resolves a mismatch.
Keep the first test small enough to reconcile by hand. When the result differs from the source documents, identify whether the problem is master data, timing, transaction ownership or configuration.
Test exceptions with the normal flow
- Planned stop definition changes
- Ideal cycle is unrealistic
- Rework is counted twice
For every exception, record the expected status, permitted action, approver and audit trail. The workflow should expose a problem without allowing an unapproved shortcut to rewrite history.
Verify the connected Optiwise workflow
Review workflow details, product capability, supporting guide, implementation context, connected process, book a demo. In the demo, ask us to run the scenario with your roles and sample records. Confirm the source transaction, resulting status, action, correction method and report.
Questions to ask before rollout
What should we test first?
Choose one current order with a known complication. Prepare the four inputs above, run the sequence and reconcile the result with the source documents.
What result should we accept?
Accept the workflow only when the normal path and named exceptions leave a complete, role-appropriate record. Keep feature validation separate from a promised outcome.
You improve OEE by reducing downtime, improving machine speed, reducing defects, tracking losses accurately, and acting on the biggest availability, performance, and quality gaps. OEE is useful only when it helps teams find practical improvement areas, not when it becomes a number on a dashboard.
OEE stands for Overall Equipment Effectiveness. It combines availability, performance, and quality. A machine can be available but slow. It can run fast but produce defects. It can produce good parts but lose too much time in setup. OEE helps separate these losses.
AICAN Optiwise helps manufacturers connect production, machine visibility, quality, maintenance, dispatch, and reporting so OEE improvement can become part of daily operations.
Understand the three parts of OEE
OEE is built on three questions:
- Availability: Was the machine available when planned?
- Performance: Did it run at the expected speed?
- Quality: Did it produce good output?
Improvement begins when teams know which part is weak.
Track downtime reasons
Availability loss usually comes from downtime.
Track:
- Machine breakdown
- Material shortage
- Setup time
- Changeover
- Operator issue
- Quality hold
- Maintenance activity
- Waiting for approval
Specific reason capture helps teams take specific action.
Track speed loss
Performance loss happens when the machine runs slower than expected.
Common causes include:
- Process instability
- Tooling issues
- Operator adjustment
- Minor stops
- Material feeding issues
- Machine condition
- Conservative speed settings
ERP and IoT dashboards can help compare planned output with actual output.
Track quality loss
Quality loss reduces usable output.
Track:
- Rejection quantity
- Rework quantity
- Defect reason
- Stage where issue was found
- Material lot or batch where relevant
- Retest or final status
OEE improves when defects are reduced, not hidden.
Use daily review, not monthly blame
OEE should support daily improvement.
Review:
- Top downtime reasons
- Machines below target
- Repeated quality issues
- Changeover losses
- Maintenance alerts
- Production plan gaps
- Action owners
This turns OEE into a management rhythm.
How Optiwise Supports the Workflow
Optiwise can help manufacturers improve OEE by connecting machine status, production plans, downtime, output, quality, maintenance, and dashboards.
A practical implementation can focus on:
- Availability tracking
- Planned versus actual output
- Downtime reason capture
- Defect and rework visibility
- Maintenance follow-up
- OEE dashboards
- Action tracking
AICAN helps manufacturers use OEE as a practical improvement system.
Founder’s Note
OEE becomes useful when it stops being a management score and starts becoming a shop-floor conversation. At AICAN, we believe OEE should show teams where capacity is leaking and what action will actually improve the day. Learn more at About AICAN.
FAQs
How can I improve OEE?
Improve OEE by reducing downtime, improving machine speed, reducing defects, tracking losses accurately, and reviewing actions daily.
What are the three parts of OEE?
OEE includes availability, performance, and quality.
Can ERP improve OEE?
ERP can support OEE by connecting production plans, output, downtime, quality, maintenance, and dashboards. IoT can add real-time machine signals.
What downtime reasons should I track?
Track breakdowns, setup, changeovers, material shortages, quality holds, operator issues, maintenance, and waiting time.
Is OEE useful for small factories?
Yes, if it is used simply and practically to find major losses and improve daily production discipline.
Related Posts
Kanban System | Optiwise
Learn how a Kanban system works in manufacturing, where it helps, where it fails, and how Optiwise connects Kanban signals with inventory, purchase, and production planning.
12 Jun 2026Read more →Erp In Operations Management | Optiwise
Learn how ERP improves operations management by connecting planning, inventory, purchase, production, quality, dispatch, finance, and reporting.
12 Jun 2026Read more →ERP for FMCG Companies in India
A practical guide to ERP for FMCG companies in India, covering distributor orders, batch tracking, expiry, inventory, production, schemes, costing, and reporting.
11 Jun 2026Read more →
Optiwise, Odoo, Acumatica and Business Central for Manufacturing
Compare manufacturing workflows in Optiwise, Odoo, Acumatica and Dynamics 365 Business Central. See what your factory can run in Optiwise.
11 Jun 2026Read more →